Engineering
Machine Vision Lighting Guide
Lighting is the highest-leverage decision in machine vision. Geometry beats intensity, and both beat software.
Direct answer
How do you choose machine vision lighting?
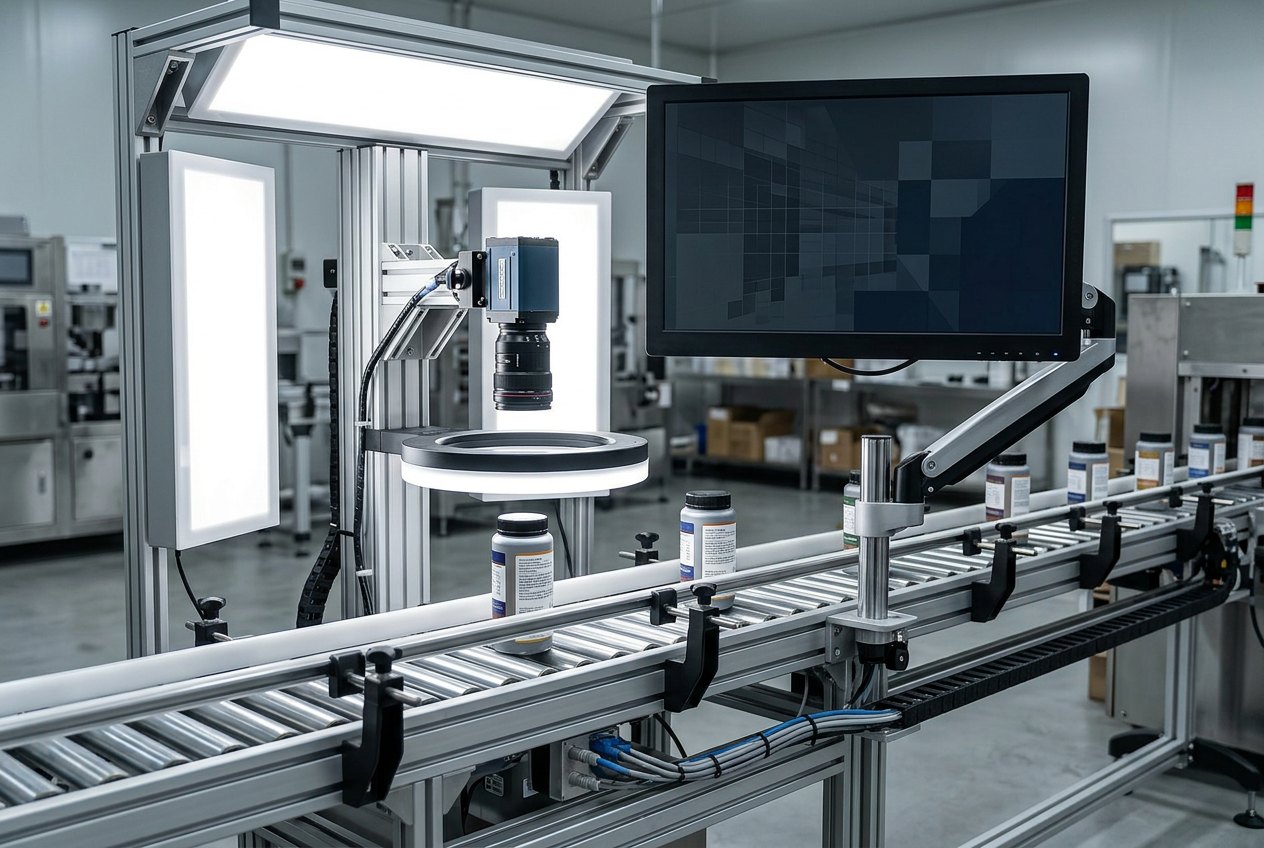
Choose the geometry that makes the defect differ from the background: backlight for silhouette and dimension, dark field or low angle for scratches and embossing, diffuse dome for specular or curved surfaces, coaxial for flat reflective parts, and polarization to suppress glare. Then set intensity and pulse duration to freeze motion at the required exposure.
Geometry catalogue
- Bright field (direct)
- General features on matte surfaces; simple, prone to hot spots
- Dark field / low angle
- Scratches, embossing, edges, wrinkles, surface texture
- Diffuse dome
- Specular, curved or foil surfaces; kills hot spots
- Coaxial / on-axis
- Flat mirror-like parts, laser marks on metal
- Backlight
- Silhouette, dimension, presence, fill level, hole detection
- Structured / line
- Height, warp, seal profile via triangulation
- Polarization
- Glare suppression on film, glass and gloss varnish
Fig. — Illumination geometry selection
Bright-field
High-contrast printed marks on matte substrate
Dark-field / low angle
Scratches, embossing, edge chips, surface texture
Backlight
Silhouette, fill level, presence, gap and edge measurement
Dome / diffuse
Glossy labels, curved bottles, reflective foil lidding
Coaxial / on-axis
Flat specular surfaces, laser marks on metal, mirror finish
Polarized
Suppressing hot-spots and glare on shrink film and gloss varnish
Practical rules
- Test lighting on real production samples, including the worst substrate, before selecting a camera.
- Pulse and overdrive rather than run continuously: more light at exposure, less heat, longer life.
- Shield ambient light. A station that works on night shift and fails at noon is an enclosure problem.
- Plan for LED aging and window contamination with a periodic reference-image check.
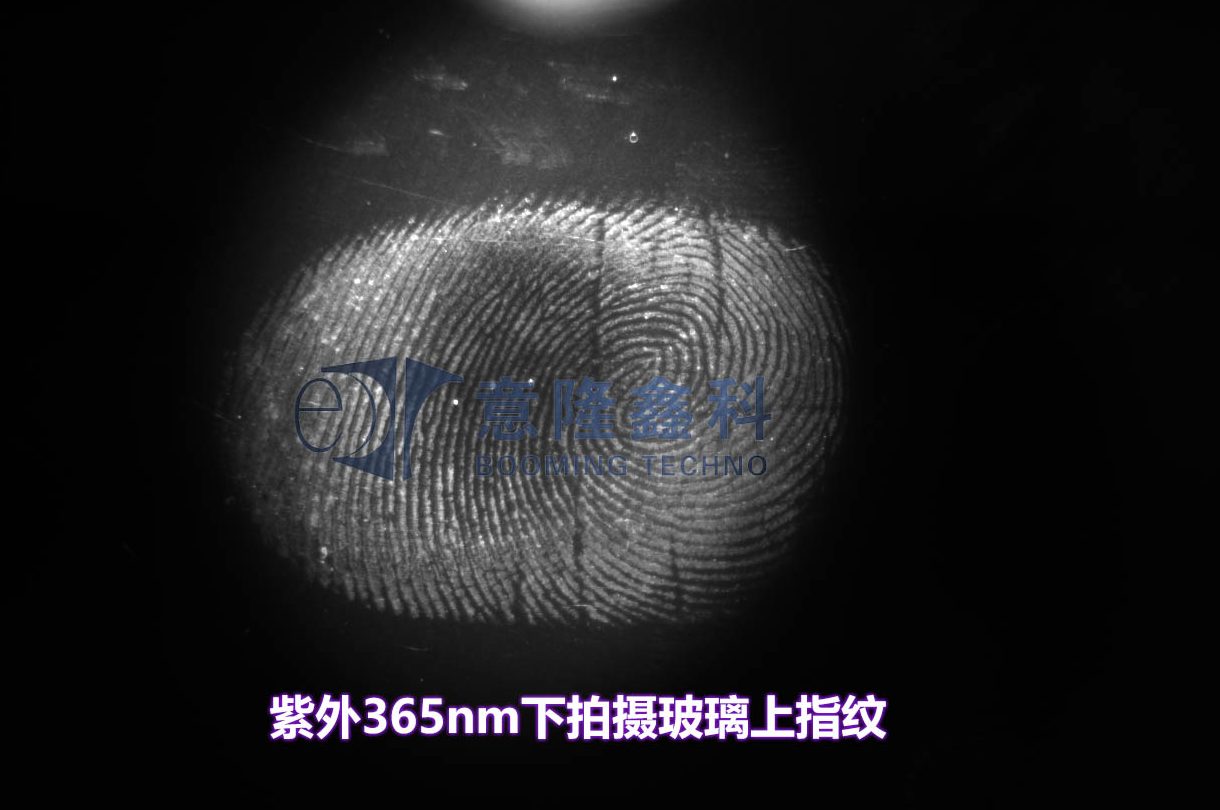
- Wavelength is a tool: red or IR can suppress color variation; blue can increase contrast on some films.
Reflective packaging and condensation
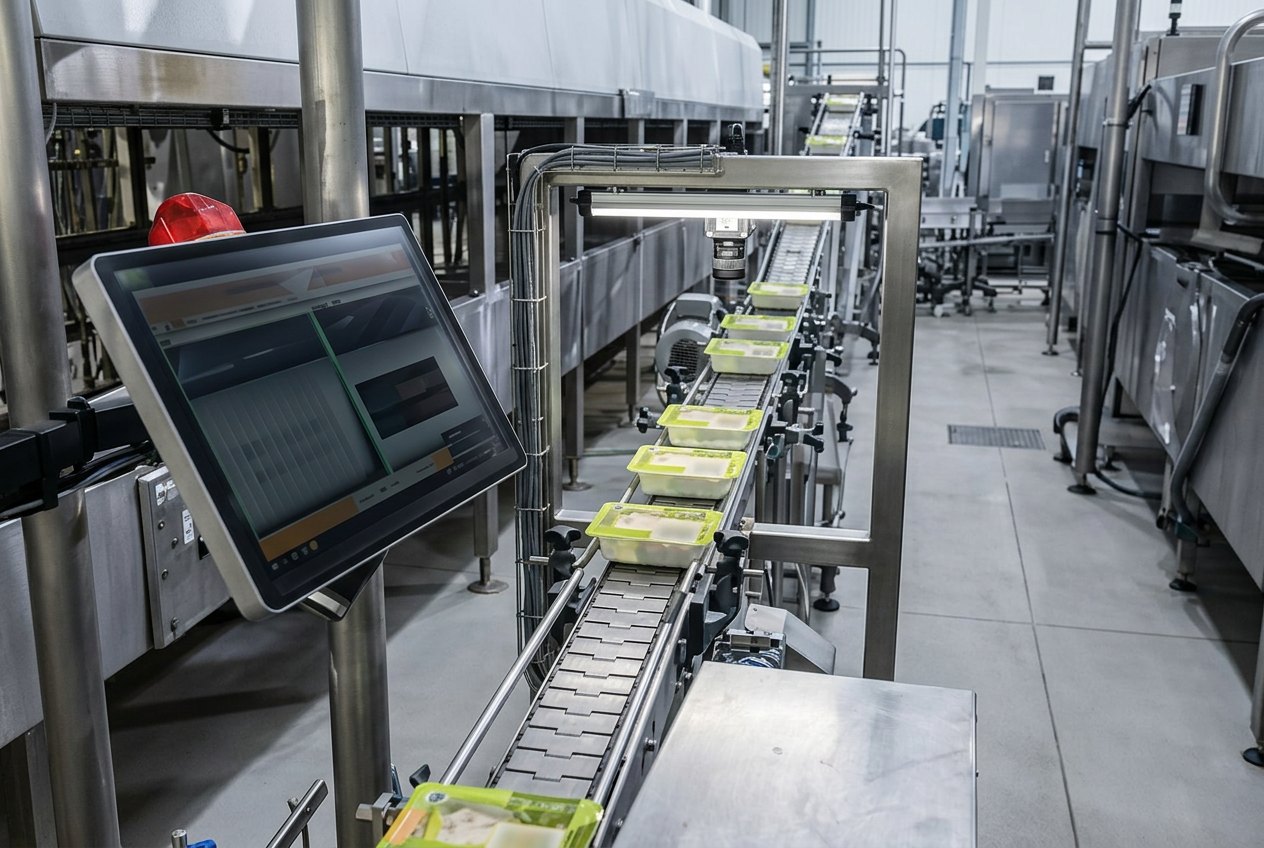
Two recurring industrial cases deserve their own note. On metallized film and gloss laminate, the objective is to keep the specular lobe out of the lens — diffuse dome, cross-polarization, or a deliberate off-axis geometry. Where product is cold and the plant is humid, condensation on the product or the enclosure window can destroy contrast; mitigation includes purge air, heated windows, enclosure sealing, and choosing an inspection point after temperature equalization.
Frequently asked questions
- Can software fix bad lighting?
- Rarely, and never for free. Software can normalize illumination that is merely uneven; it cannot recover contrast that was never captured. Fixing lighting is almost always the cheaper intervention.
- How do I inspect a shiny curved bottle?
- Diffuse dome or tunnel illumination to spread the reflection, often combined with restricting the region of interest to a stable band, or multiple cameras around the part.
Related engineering material